 Skip to content

Description
Carbon Fibre PA6 (Nylon) 3D Printing Filament
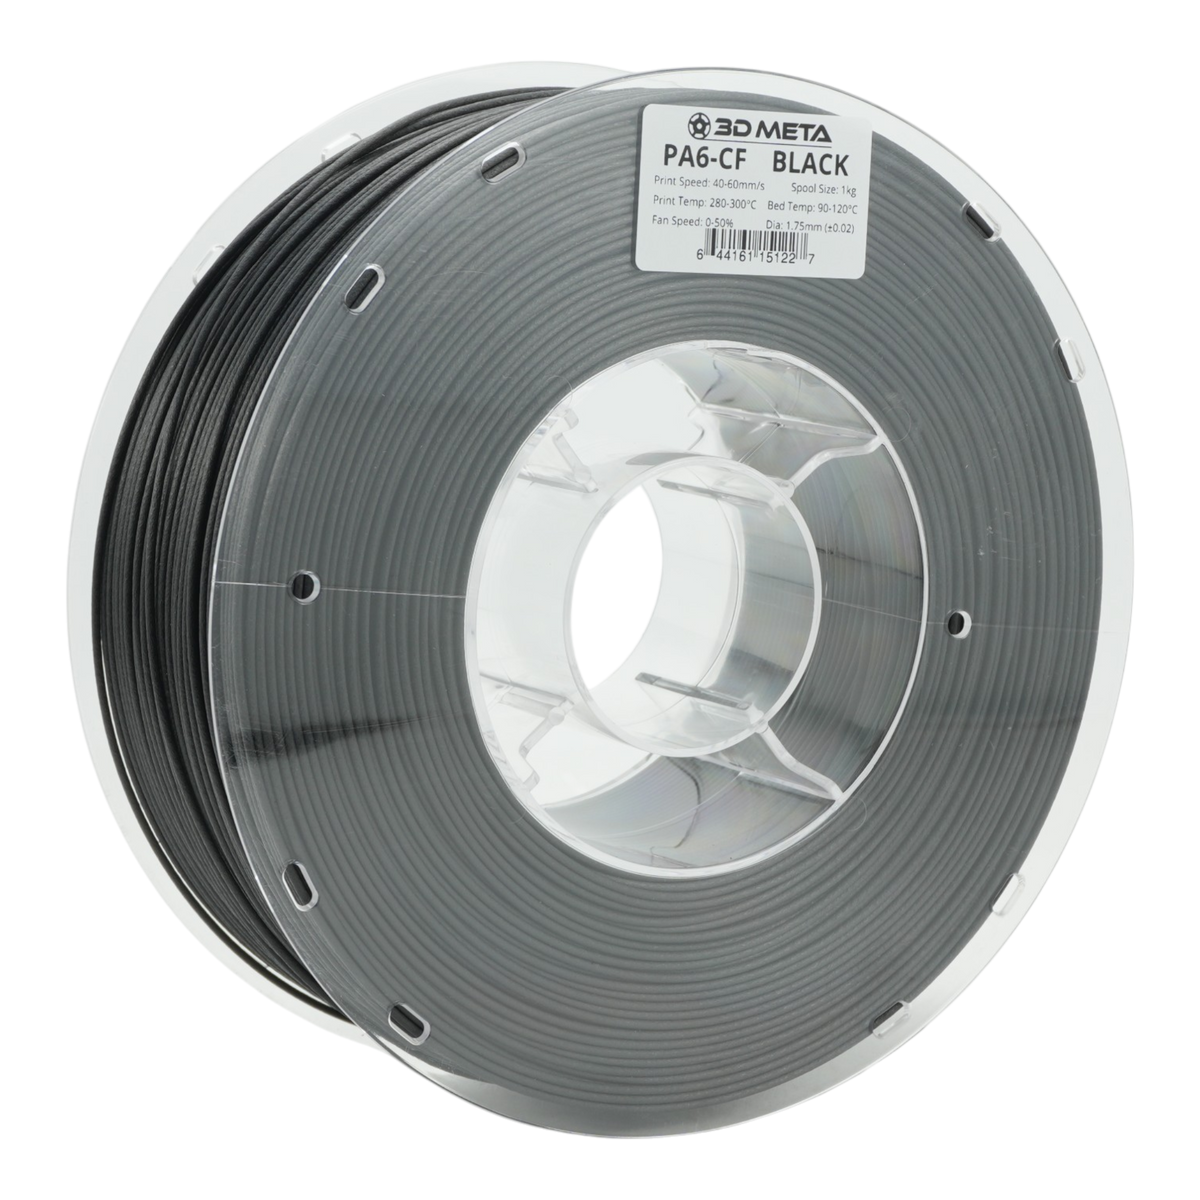
3D META's PA6-CF 3D printing filament combines the toughness of PA6 nylon with 10% chopped carbon fibre, producing parts with outstanding stiffness, strength and heat resistance. With a heat deflection temperature of around 200°C and a flexural modulus more than four times that of standard PLA, PA6-CF is the material to reach for when a part has to carry real load in a hot environment — brackets, mounts, jigs, drone frames and under-bonnet components. Like all 3D META filaments, it is manufactured to strict quality standards and supplied on a recyclable plastic spool.
Key Features of PA6-CF 3D Printing Filament
- Exceptional Stiffness and Strength: Carbon fibre reinforcement delivers a flexural modulus of 4,300–4,800 MPa and tensile strength of 63–67 MPa — ideal for structural, load-bearing parts.
- High Heat Resistance: Heat deflection temperature of 200°C (0.455 MPa) and a continuous use temperature of 150°C, so parts hold their shape near engines, heaters and hot enclosures.
- Dimensional Stability: Carbon fibre dramatically reduces the warping and shrinkage of unfilled nylon, giving accurate, flat prints.
- Matte Engineering Finish: Prints with a smooth, matte, fibre-flecked surface that hides layer lines.
- Strong Layer Adhesion: Excellent inter-layer bonding for durable, fatigue-resistant parts.
- Strict QA Manufacturing: Every batch is checked for diameter, fibre dispersion and print performance.
Applications for PA6-CF 3D Printing Filament
- Structural Brackets and Mounts: Rigid components that must carry load without flexing.
- Jigs, Fixtures and Tooling: Durable workshop tooling that holds tolerance under repeated use.
- Automotive and Under-Bonnet Parts: Heat-resistant housings, ducts and brackets.
- Drone and RC Frames: Light, stiff frames and arms with high impact tolerance.
- Industrial End-Use Parts: A practical alternative to machined nylon or aluminium for low-volume production.
Note: PA6-CF is abrasive and hygroscopic. Use a hardened steel or wear-resistant nozzle, dry the filament before every print, and print from a dry box or dryer for best results. An enclosed printer is strongly recommended.
Storage and Drying for PA6-CF Filament
PA6 absorbs moisture quickly, and wet nylon prints with bubbles, stringing and poor strength:
- Store in a Cool, Dry, Dark Environment: Keep the spool vacuum-sealed or in an airtight container with fresh desiccant at all times.
- Dry Before Every Print: Use a filament dryer, food dehydrator or enclosed 3D printer at 80°C for a minimum of 12 hours.
Why Choose 3D META's PA6-CF 3D Printing Filament
- Engineering-Grade Performance – Verified mechanical and thermal data (see Technical Specs) so you can design with confidence.
- Top-Quality Materials – Premium PA6 resin with evenly dispersed carbon fibre for consistent extrusion and strength.
- Strict QA Standards – Tight diameter tolerance and verified print performance, batch after batch.
- Fully Tested In-House – Every batch is print-tested on real engineering geometries before release.
- Local Support – Australian stock, fast shipping and help from people who print with it.
Need maximum stiffness and heat resistance? Order 3D META PA6-CF filament today. Looking for lower moisture absorption and better chemical resistance instead? See our PA12-CF filament.
Print Settings
Recommended starting settings for 3D META PA6-CF filament. Every printer is different — treat these as a guide and tune for your machine.
| Setting | Recommended |
|---|---|
| Nozzle Temperature | 270–290°C |
| Bed Temperature | 60–90°C |
| Print Speed | 40–60 mm/s |
| Part Cooling Fan | 50–100% |
| Layer Height | 0.12–0.3 mm |
| Retraction Distance | 4–6 mm |
| Retraction Speed | 40–60 mm/s |
| Nozzle | Hardened steel or wear-resistant, 0.4 mm or larger |
| Print Surface | Most print surfaces e.g. Glass, META FLEX etc |
| Printing Environment | Room Temperature – 50°C (enclosure recommended) |
| Support Material | PVA |
| Drying (before printing) | 80°C for a minimum of 12 hours |
Technical Specs
| Property | Test method | Value |
|---|---|---|
| Filament | ||
| Material | PA6 (Nylon) with 10% carbon fibre | |
| Diameter | 1.75 mm (±0.02 mm) | |
| Net weight | 1 kg | |
| Colour | Black | |
| Spool | Recyclable plastic spool | |
| Physical Properties | ||
| Density | ISO 1183 | 1.24–1.26 g/cm³ |
| MFR (250°C / 2.16 kg) | ISO 1133 | 3–6 g/10 min |
| Moisture Absorption | ISO 62 | <0.3% |
| Mechanical Properties | ||
| Tensile Strength | ISO 527 | 63–67 MPa |
| Elongation at Break | ISO 527 | 16.5–17.5% |
| Flexural Modulus | ISO 527 | 4300–4800 MPa |
| Flexural Strength | ISO 178 | 140–145 MPa |
| Impact Strength | ISO 179 | 11.5–13.5 kJ/m² |
| Thermal Properties | ||
| HDT @ 0.455 MPa (66 psi) | ISO 75 | 200°C |
| Continuous Use Temperature | IEC 60216 | 150°C |
| 200-hour Continuous Test | 180°C | |
Download the full PA6-CF Technical Data Sheet (PDF).
FAQ's
Q: Do I need a special nozzle for printing with PA6-CF filament?
A: Yes. Use a hardened steel or other wear-resistant nozzle. The carbon fibre content will quickly wear out a standard brass nozzle, widening the orifice and ruining dimensional accuracy.
Q: What is the main difference between PA6-CF and PA12-CF?
A: PA6-CF is the stiffer, stronger and more heat-resistant of the two (HDT 200°C vs 90°C), making it the better choice for structural parts and hot environments. PA12-CF absorbs less moisture, has better chemical resistance and is more dimensionally stable, so it is easier to print and better suited to parts exposed to oils, fuels or humidity.
Q: Do I need an enclosed printer?
A: Strongly recommended. PA6 is prone to warping on open-frame printers; a heated enclosure keeps the part warm and greatly improves layer adhesion and flatness.
Q: How should I store PA6-CF filament?
A: Store it vacuum-sealed or in an airtight container with desiccant, and dry it at 80°C for at least 12 hours before printing. PA6 absorbs moisture within hours of being exposed to air, so printing from a dry box or active dryer gives the most consistent results.